News
DIRECT ANSWER
GOB coating adds separate blocks of time after the module leaves the coating machine: curing, inspection, and — when a module fails — rework or a scrap decision. Those blocks do not disappear because the coating step itself was fast, and they do not run in parallel with coating the next batch unless you plan the sequence deliberately. A realistic delivery date counts every block: coat, cure, inspect, and the buffer for the first article and for any rework. Promise the date the batch is released, not the date it is coated.
A bare LED module becomes a shippable GOB-coated module in four stages, and each stage has its own owner, its own waiting, and its own way to go wrong.
| Block | What happens | What decides how long it takes | What to prepare in advance |
|---|---|---|---|
| 1. Coating | The machine applies the glue layer over the module face | Module size, glue path program, and whether the program and fixture are already proven for this module | A stored program with the right name, a fixture that is seated, and the correct glue batch identity |
| 2. Curing | The glue layer hardens at room temperature until the module is safe to move, test, and pack | The glue's own datasheet: mix ratio, layer thickness, and workshop temperature | A curing area that is free, labelled, and separate from the coating station |
| 3. Inspection | The coated module is checked before it moves on — coverage, edges, visible bubbles, and a power-on check | Your customer's acceptance standard and how many modules you inspect per batch | The inspection criteria written down before the batch starts, not invented during it |
| 4. Release and packing | Passed modules are packed for shipment or fitted into cabinets | Whether any module failed inspection and needs a rework decision | Packing material and labels ready, so a passed batch does not wait for packaging |
The first block is the only one the coating machine controls. The other three are planning blocks. A delivery promise that counts only the first block is wrong by the sum of the other three.
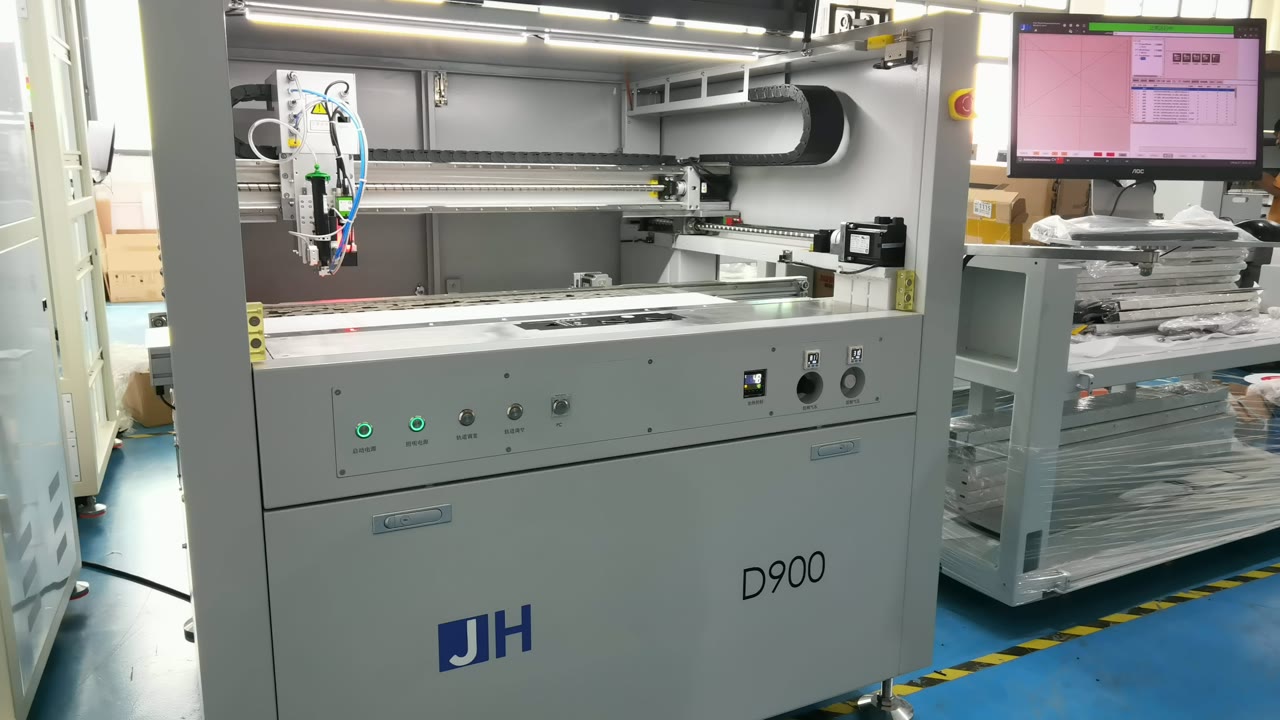
JH-D900 precision dispensing machine — a dispensing reference, not a GOB coating machine. The coating step is only the first block of GOB lead time; curing, inspection and rework follow.
Curing is the easiest block to underestimate, because nothing visible happens while it runs. The module sits still, the glue hardens, and the line looks idle. Three facts from the glue's own material data explain why this block cannot be compressed by wishing:
Curing time follows the mix and the temperature, not the schedule. For the OPT315 silicone used in JHIMS GOB work, the two components mix at a general weight ratio of A:B = 10:1, and more of component B shortens both the curing time and the working time. A higher workshop temperature also speeds curing. That cuts both ways: a cold morning stretches the block, and a hot afternoon shortens the working window for the glue itself.
Thickness changes the job. A potting layer below 20 mm can defoam naturally without separate defoaming; a thicker layer may trap pinholes or bubbles inside, so the mixed glue should be vacuum-defoamed for at least 5 minutes at 700 mmHg before it reaches a module. That step belongs in the plan, not in the gap between batches.
Do not heat the cure to save a day. The OPT315 material data states plainly that heating curing is generally not recommended, because it can cause pinholes or bubbles on the surface and inside the layer and affect appearance and sealing. A batch "saved" by heating is a batch that may fail inspection — and then costs more days than it saved.
The practical rule is simple: treat curing as its own dated block in the plan, with a named start (when the last module of the batch is coated) and a named release condition (the glue's datasheet condition is met and the module passes its handling check). Until that condition is met, the batch is not shippable, however good it looks. The handling rules for this waiting period — what a module may and may not do while it cures — are covered in our companion piece on curing, handling, and storage after GOB coating.
Curing time is only dead time if one batch occupies the whole line. The coating machine finishes a batch and moves on; the curing area holds the finished batch while the machine starts the next one. That overlap is where realistic planning recovers most of the lost day, but it only works if three conditions hold:
1. The next batch is ready to coat. Its program is loaded and proven, its fixture is seated, and its glue batch is verified. If any of those checks is still open when the machine finishes the first batch, the machine waits — and the overlap is lost.
2. The curing area is separate from the coating station. Coated modules must leave the machine's work area to a labelled curing space. If they stay on the machine table "just until they set," they block the next batch and the plan collapses into a single file.
3. One variable changes at a time. If the next batch uses a different module size, a different program, or a new glue batch, that change is verified on its own — a first article, a program check, a glue identity check — before the batch runs. Stacking two changes on the first batch of the day is how a planning gain turns into a rework day.
A useful way to lay this out is a simple two-row plan for each production day: which batch is on the machine, and which batch is curing. If the curing row is empty, the machine is the only thing working. If the machine row is empty, the curing row is the only thing working. The day is planned well when neither row is empty for long.
Two moments in every GOB run deserve their own time in the plan, because both are decision points, not formalities.
The first article. Before a batch runs, one module is coated first and checked — coverage, edges, uniformity, and visible bubbles — to decide whether to follow, adjust one thing and repeat, or stop the batch. That check is the cheapest inspection in the whole job: it costs one module and a few minutes, and it can save a full batch. A plan that skips it to save time has not saved time; it has moved the risk to the end of the batch, where it is most expensive. The same discipline applies before coating starts at all: inspect the bare module first, so coating does not lock in a defect that was already there.
A new glue batch. When a batch of modules changes to a new glue batch midway, the new batch must be verified before it is used, and the traceability record must split at that point so modules coated before and after the change can be told apart. That verification and the record split are small jobs, but they are jobs — they belong in the plan as their own lines, not as interruptions discovered halfway through a shift.
Both moments are also the points where a good record pays for itself. If a customer later asks why a batch was late, or why a module was held, the record shows the decision and the reason. If there is no record, the conversation starts from zero.
Some modules will fail inspection. That is not a planning failure; it is the reason inspection exists. What turns it into a delivery failure is a plan with no room for it.
When a coated module fails, the decision is repair or scrap, and that decision needs evidence: what the defect is, where it is, which glue batch and program coated it, and whether the same defect appears on neighbouring modules. Our companion piece on reworking a GOB-coated module works through that decision. For planning purposes, the point is narrower: the decision takes time, the rework takes time, and the re-inspection after rework takes time. None of that time exists in a plan that assumes every module passes first time.
A workable approach is to promise the customer a release date that already contains a rework allowance, and to keep that allowance visible inside the factory as "held for decision" rather than quietly absorbing it by skipping inspection. Skipping inspection to protect a date does not protect the date — it moves the failure to the customer's site, where it costs a return, a replacement batch, and the next order.
A delivery promise for GOB-coated modules should name the release date, not the coating date. Three sentences cover most situations:
"Your modules are coated on [date] and released after curing and inspection on [date]." The second date is the promise.
"If inspection holds any modules, we will tell you how many and what we are doing about them before the release date, not after it." A hold disclosed early is a delay; a hold disclosed late is a broken promise.
"The first batch of a new module size carries a first-article check; we will confirm the release date once that check passes." A new size is the one case where a fixed date given before the first article is a guess, and it should be labelled as one.
None of this requires quoting a price or a speed the factory has not demonstrated. It requires only that the date you give is the date the batch is genuinely ready to leave.
| Check | Question to answer | If the answer is "not yet" |
|---|---|---|
| Program and fixture | Is the program stored under the right name and the fixture seated for this module size? | Do not start the clock; run the changeover checks first |
| Glue identity | Is the glue batch verified, in date, and recorded against this module batch? | Verify and record before coating |
| Curing space | Is there a labelled curing area free for this batch, separate from the machine? | Free the space or move the date |
| Inspection criteria | Are the pass, rework, and hold criteria written down before the batch starts? | Write them; do not decide them module by module |
| First article | Is one module coated and checked before the batch runs? | Coat and check it first |
| Rework allowance | Is there time after inspection for a repair-or-scrap decision and a re-inspection? | Add it to the promised date |
| Packing readiness | Are packing materials and labels ready for the released batch? | Prepare them while the batch cures |
Promising same-day shipment of a coated batch. Coating is one block. Curing and inspection are separate blocks, and they do not finish on the same day just because the coating did.
Counting curing as overlapping coating on the same machine. Curing overlaps the next batch's coating, not the same batch's. The batch being coated now still has to wait.
Assuming the first batch of a new size runs at full speed. The first article, the fixture check, and the program check are part of the first batch's time, not overhead to be ignored.
Skipping inspection to save a day. The day is not saved; the defect is shipped, and the cost returns as a complaint, a return, or a lost order.
Heating the cure to recover a lost day. The material data advises against it, and a bubbled coating fails inspection — the recovery costs more than the delay. Stable air pressure matters for the same reason: a pressure dip during coating creates defects that inspection then has to catch, and that costs the day twice.
Letting the curing area become the packing area. A module that is moved, stacked, or packed before it is released is a module whose curing and inspection records no longer match what was shipped.
Q1: How much extra time does GOB coating add to a module order?
There is no single number. It depends on the glue's curing condition, the layer thickness, the workshop temperature, the inspection scope your customer requires, and whether the first article or a glue-batch change falls inside the run. Plan it as four blocks — coat, cure, inspect, release — and date each one from the glue's datasheet and your customer's acceptance standard, not from a rule of thumb.
Q2: Can we coat the next batch while the first one cures?
Yes — that is the normal way to keep the line busy — provided the curing area is separate from the machine, the next batch's program, fixture, and glue batch are already verified, and only one change is introduced at a time. If any of those is not ready, the machine waits and the overlap is lost.
Q3: The customer wants the modules the day after coating. Is that possible?
Only if curing, inspection, and packing can genuinely finish by then for that glue, that thickness, and that acceptance standard. If they cannot, the honest answer is the release date, given before the order is confirmed — not a coating date presented as a delivery date.
Q4: What should we do when inspection holds part of a batch?
Hold the affected modules, record the defect, the glue batch, and the program, and decide repair or scrap on evidence — not on the delivery date. Tell the customer how many modules are held and what happens next before the promised release date passes.
Q5: Does a faster coating machine shorten lead time?
It shortens the coating block only. Curing, inspection, and rework do not get faster because the machine does. A faster machine helps most when the plan already overlaps curing with the next batch's coating — then the machine is never the bottleneck.
GOB coating does not add one delay to a module order; it adds a sequence — coating, curing, inspection, and release — and each step has its own clock. Plan all four, overlap curing with the next batch's coating, protect time for the first article and for rework, and promise the release date. The factory that does that delivers late less often than the factory that promises the coating date and hopes the rest takes care of itself.
JHIMS products mentioned in this article
The GOB-LXS330 glue dispensing machine for LED displays applies the coating layer. Its published specifications include ±0.05 mm running accuracy, a 200 mm/s running speed, a 30 L glue capacity, a 0.5–0.8 MPa input pressure range, a Panasonic PLC with touch screen, parameter storage for different products, a teaching program, an anti-drip valve, and a liquid level sensing alarm. Parameter storage matters for planning: a repeat order reloads the same program instead of starting from setup. The OPT315 two-component silicone is the glue whose material data sets the curing rules used in this article — a general A:B mix ratio of 10:1 by weight, natural defoaming for layers below 20 mm, vacuum defoaming for at least 5 minutes at 700 mmHg for thicker layers, and no heated curing. The JH-D900 precision dispensing machine is cited only as a dispensing reference: its ±0.02 mm repeat accuracy and ±0.005 mg weight control describe precision dispensing in general, not a GOB coating machine. For a full view of the GOB solution, see the GOB LED display solutions page.
For technical questions about GOB coating planning, or to discuss a GOB coating machine for your module sizes, contact JHIMS at [email protected].


 Teams
 whatsapp
 telegram
